Custom Soap Mold Design Guide
Design custom silicone soap molds around soap process, bar or loaf geometry, target weight, logo detail, release, tray support, multi-cavity layout and prototype validation.
 Kyler Yang · Founder8 min read
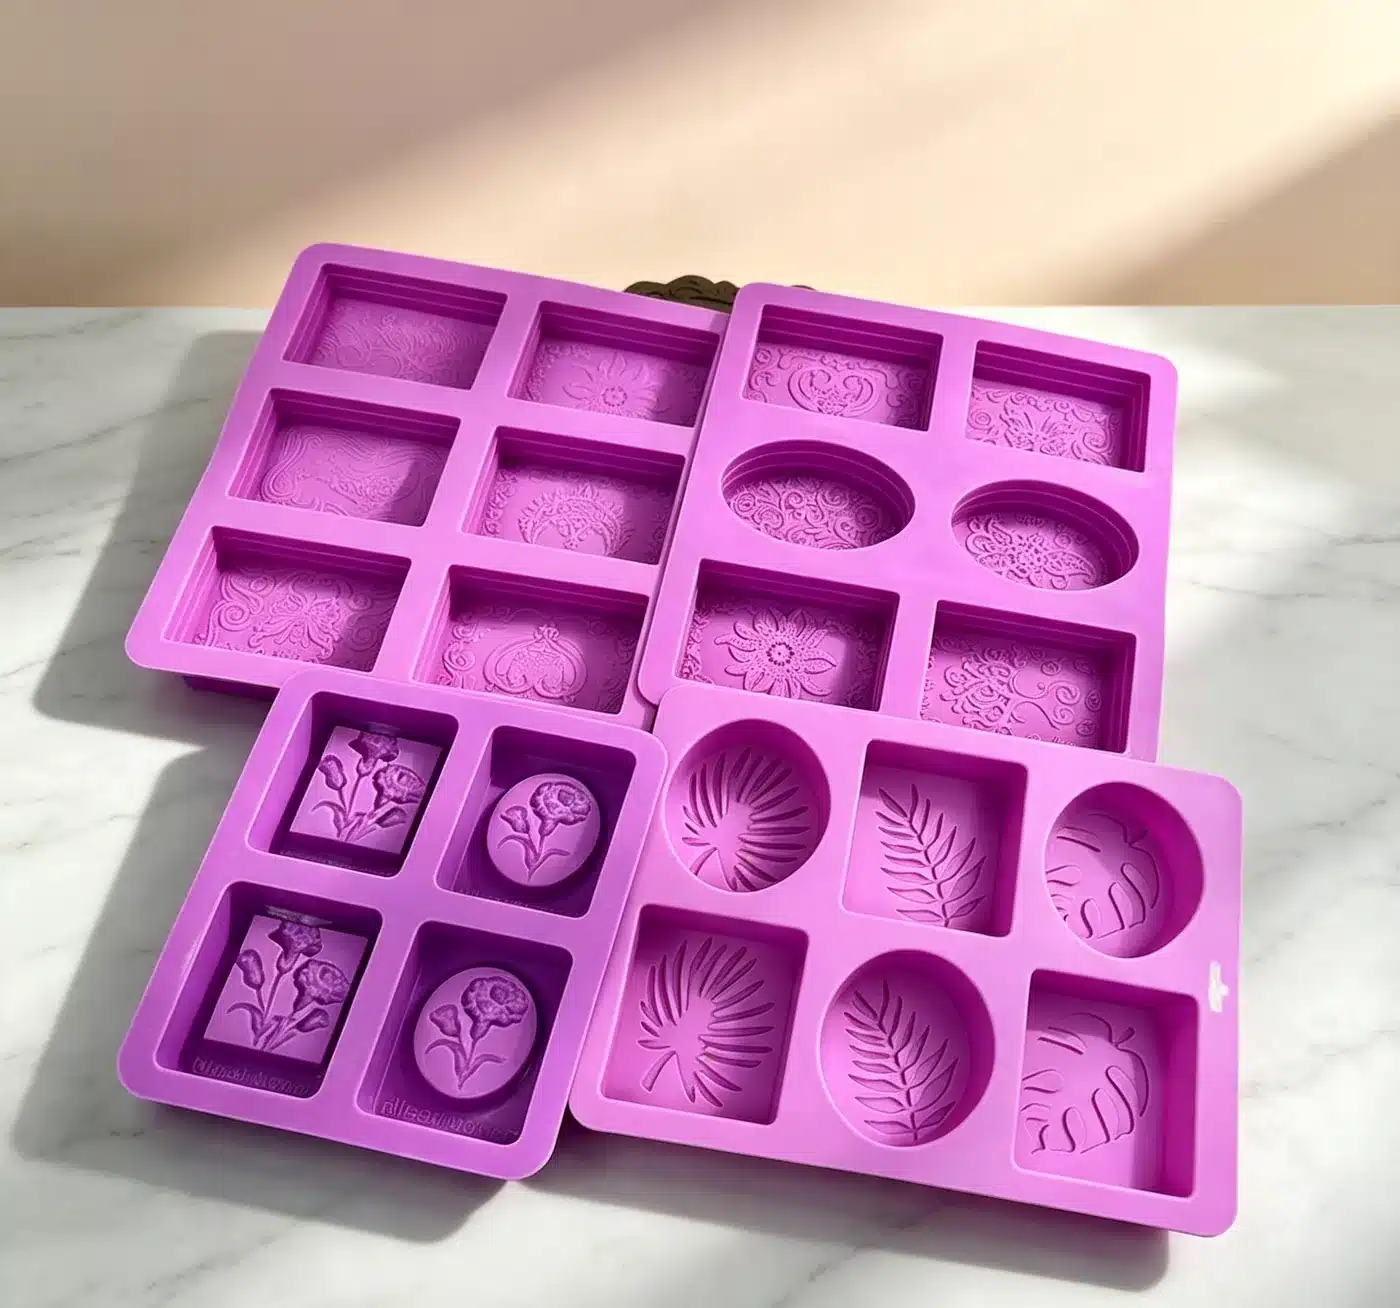
A soap mold should be designed around the soap process + finished product + demolding method.
The same silicone geometry will not necessarily perform the same way with cold-process soap, melt-and-pour soap and a deeply detailed decorative bar.
Start with the finished soap and the production workflow, then decide the mold structure.
1. Bar Cavity or Loaf?
Individual Bar Cavities
Best when each cavity forms the finished bar shape.
Design questions:
- target bar dimensions;
- weight reference;
- logo/texture;
- release direction;
- cavity count;
- tray support.
Loaf Mold
Best when a larger block is poured and cut later.
Design questions:
- internal loaf dimensions;
- batch mass;
- support box/frame;
- liner removal;
- cutter/portion plan.
The cavity geometry does not directly determine final bar weight if the loaf is cut afterward.
2. Define Which Weight Matters
For cold-process soap, the buyer may talk about:
- fresh-pour weight;
- demolded weight;
- cured/sale weight.
These are not necessarily identical because the formula can lose water during cure.
For a cavity mold, the initial volume can be designed around a target, but validate the actual formula before treating CAD volume as guaranteed sale weight.
For a loaf mold, weight also depends on the cut plan.
3. Release Geometry Comes Before “Soft Silicone”
Ask:
- Is the bar flat-backed?
- Does it have rounded return edges?
- Are there deep side details?
- Does the logo create isolated islands?
- Is the product strong enough to flex out of the cavity?
- Can the operator peel the mold without twisting the bar?
A simple flat-back bar may work with an open cavity.
A fully sculpted or undercut design may need:
- a split;
- slit;
- plug/core;
- another controlled opening.
The right structure can reduce the amount of stretching required from the silicone.
4. Logo Depth and Fine Text
For a logo or lettering, review:
- real finished size;
- smallest stroke;
- spacing;
- depth;
- internal counters;
- corner shape;
- product thickness behind the detail.
Fresh soap can be softer and more vulnerable to smeared or broken detail than a rigid casting.
Do not copy one minimum stroke or depth from another project.
Prototype the actual brand mark at production size.
5. Multi-Cavity Layout
A 12-, 16- or 20-cavity request should be treated as a loaded production tray, not only a CAD grid.
Review:
- outside dimensions;
- cavity arrangement;
- inter-cavity support;
- filled mass;
- movement from fill to cure area;
- operator demolding sequence;
- rack/table constraints.
A very large soft tray can become difficult to carry even if each individual cavity is easy to release.
6. Mold Support
Possible support approaches can include:
- thicker perimeter geometry;
- external rigid board/pan;
- support box;
- rigid shell for sculptural molds;
- smaller tray modules.
The correct approach depends on the mold.
A harder silicone does not automatically replace good support design.
7. Process and Formula Inputs
For useful DFM, tell the supplier:
- cold process / hot process / melt-and-pour;
- pour temperature where relevant;
- fragrance/additive conditions that matter;
- expected demold time/process;
- cleaning;
- batch size.
Material compatibility should be checked for the selected formulation and use.
Do not assume one soap formula proves compatibility with all soap products.
8. Master and Surface Finish
The silicone mold reproduces the master.
Check the master for:
- scratches;
- print lines;
- machining marks;
- seams;
- texture;
- logo edges;
- intentional matte/gloss finish.
If the finished soap needs a specific appearance, approve the master surface before molding.
9. Prototype the Real Workflow
A prototype should test:
- fill;
- bar/loaf dimensions;
- target weight reference;
- logo;
- release;
- mold stress;
- tray stability;
- cleaning;
- operator handling.
For difficult CP recipes, use the real formula where possible.
Do not approve the design only because the empty mold looks correct.
10. Record the Approved Revision
At approval, record:
- drawing/CAD revision;
- bar/loaf dimensions;
- logo version;
- cavity count;
- material;
- support method;
- approved soap/process;
- sample reference.
This makes repeat orders and future SKU changes easier to control.
Common Problems
The Logo Tears or Smears
Investigate:
- soap condition at demold;
- excessive depth;
- fine unsupported strokes;
- undercut;
- demolding method.
The Tray Feels Too Floppy
Investigate:
- filled mass;
- span;
- support;
- web/perimeter design;
- selected material.
Bar Weight Is Off Target
Investigate:
- which weight stage is being compared;
- actual formula density/water loss;
- fill consistency;
- cavity volume;
- tray deformation.
A Decorative Bar Will Not Release
Investigate:
- return edges/undercuts;
- parting/split strategy;
- bar strength;
- peel direction.
Frequently Asked Questions
What Shore A should a soap mold use?
There is no universal answer. Material properties, geometry, support and the actual demolding process need to be considered together.
How many bars should one tray contain?
Use the production workflow to decide. A larger tray can increase cavity count but also increase filled weight and handling difficulty.
Can a soap logo be very deep?
Deeper is not always better. Fine/deep features can make filling and demolding harder.
Can I design from final retail bar weight?
Use it as a target, but clarify the formula and whether the weight is measured fresh, at demold or after cure.
Commercial Next Step
For a quotation:
Custom Silicone Soap Molds /products/custom-silicone-soap-molds/
Custom silicone development · DFM & prototype support
CAD, drawing, photos or sample details